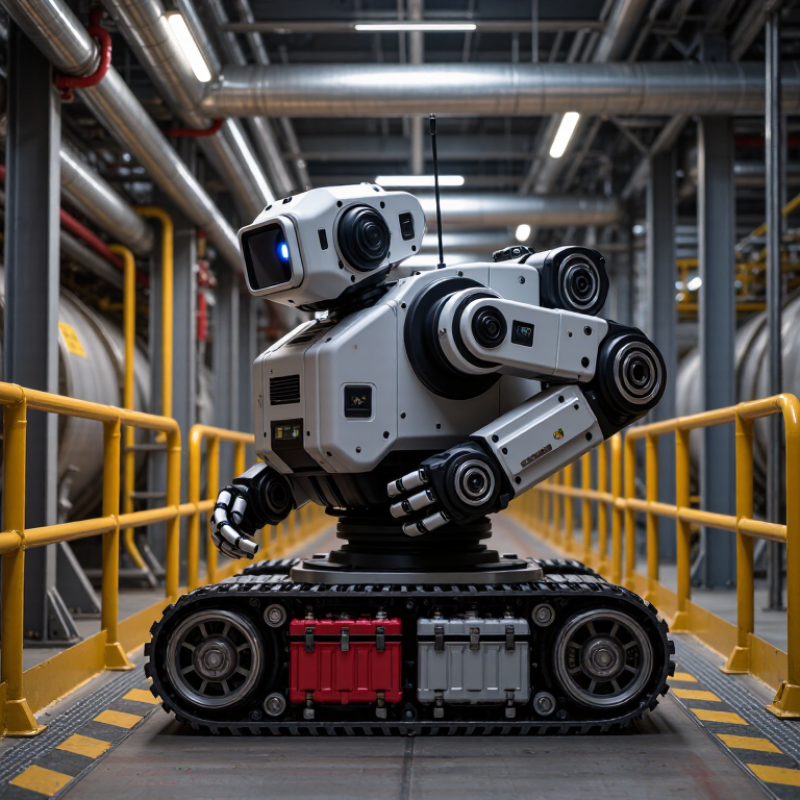
Choosing the China Best Explosion-Proof Robot Manufacturer? The answer requires more than comparing factory prices or polished product photos. A reliable evaluation must examine certification, field experience, engineering depth, and after-sales support. These factors matter when robots enter refineries, chemical plants, mines, or storage areas containing flammable gases and dust.
Sander van der Meer, founder of ExRobotics, has stated, “Safety comes before productivity.” This principle captures the real purpose of an Explosion-Proof Robot. The machine must reduce human exposure without creating another ignition risk. Its enclosure, motors, batteries, sensors, and communication systems should be designed for hazardous environments. Independent testing and traceable documentation are essential.
Look closely at the details. Can the robot inspect narrow pipe corridors? Can it transmit stable video beside steel tanks? Does its battery remain controlled after long patrols? A dependable manufacturer should explain protection methods, operating limits, maintenance intervals, and certification scope in plain English. Factory audits, customer references, and documented field trials provide stronger evidence than advertising claims.
Experience also reveals uncomfortable gaps. Some manufacturers may offer impressive prototypes but limited deployment records. Others may provide certificates without enough technical explanation. No ranking is perfect. That weakness deserves attention.
This guide compares Chinese suppliers through practical criteria, including product reliability, customization ability, manufacturing controls, inspection performance, and service response. The strongest candidate is not always the cheapest. It is the company that can prove consistent safety, repeatable quality, and useful performance under demanding industrial conditions. Still, buyers should verify every claim independently before selecting an Explosion-Proof Robot for their facility.
Explosion-proof robots are engineered for areas where flammable gas, vapor, or dust may create ignition risks. Their protected housings reduce sparks, heat, and electrical faults escaping into the surrounding atmosphere. However, “explosion-proof” is not a universal label. Equipment must match the site’s hazard classification, temperature limits, and certification requirements.
These robots support inspection, material handling, cleaning, and remote monitoring in chemical plants, fuel storage areas, paint facilities, and dusty processing workshops. A robot can enter narrow corridors, inspect warm pipelines, or carry cameras near equipment that workers should not approach routinely. Reliable systems also require sealed joints, controlled motor temperatures, suitable cables, and emergency shutdown functions. In practice, a robot may look robust but still fail if its sensors, charging station, or accessories are unsuitable. That detail is often overlooked.
Tips: Check certification before performance claims. Confirm gas or dust group compatibility. Test communication in metal structures. Ask for maintenance records and operator training details. Also, review local safety requirements with a qualified engineer. Small gaps matter. No robot removes every hazard. A careful risk assessment should guide deployment, even when the machine performs well during factory testing.
China Best Explosion Proof Robot Manufacturer?
Safety Standards for Explosion-Proof Robot Manufacturing in China
A reliable explosion-proof robot starts with a documented hazard assessment, not a modified standard robot. Manufacturers should identify gas, vapor, dust, or fiber risks around each operating area. The zone classification determines the required protection method, equipment group, temperature class, and enclosure design. In China, the GB/T 3836 series is central to equipment used in explosive atmospheres. It closely follows relevant IEC 60079 principles. Product certification requirements must also be checked for the intended application.
During factory audits, engineers should examine motors, connectors, cable glands, sensors, batteries, and control cabinets separately. Small gaps matter. Sealing surfaces need accurate machining and careful inspection. Grounding paths should be tested, while electrostatic accumulation requires practical control. The robot’s movement can create heat, friction, and unexpected cable stress. These factors belong in the risk assessment. A certificate alone is not enough.
Manufacturers should provide material records, inspection reports, test evidence, and clear maintenance instructions. Independent laboratory testing can verify flameproof joints, temperature rise, ingress protection, and electrical safety. Factory acceptance testing should include realistic loads and operating cycles. We have seen designs pass paperwork reviews but struggle with field maintenance. That weakness deserves attention. Spare parts must preserve the original protection level, and technicians need training before entering hazardous areas. Continuous improvement is necessary because real plants rarely match drawings perfectly.
| Safety Dimension | Applicable Standard or Framework | Key Manufacturing Requirement | Recommended Verification Evidence | Typical Application Consideration | Compliance Status |
|---|---|---|---|---|---|
| Hazardous-Area Classification | GB 50058-2014; IEC 60079-10-1; IEC 60079-10-2 | Identify the explosive gas, vapor, mist, or combustible dust hazard before selecting the robot protection concept. The classification must define the applicable zone and operating conditions. | Approved area-classification drawings, process hazard data, zone designation, and site risk assessment. | Gas zones commonly include Zone 0, Zone 1, and Zone 2. Dust zones commonly include Zone 20, Zone 21, and Zone 22. | Required before design |
| Equipment Group and EPL | GB/T 3836 series; IEC 60079 series | Match the robot and all associated equipment to the required Equipment Protection Level, gas or dust group, and hazardous-area classification. | Ex marking review, certification documents, product technical file, and equipment selection record. | Equipment for a higher-risk zone generally requires a protection level appropriate to that zone; the final selection depends on the complete installation assessment. | Mandatory design input |
| General Explosion-Protection Requirements | GB/T 3836.1-2021 | Control ignition sources, temperature, electrical clearances, mechanical construction, materials, fasteners, cable entries, and marking for equipment used in explosive atmospheres. | Design calculations, material certificates, drawings, component lists, temperature-rise tests, and construction inspection records. | Applies as the general foundation for equipment using one or more recognized protection methods. | Core requirement |
| Flameproof Enclosure Protection | GB/T 3836.2-2021; IEC 60079-1 | Use certified flameproof joints, enclosure dimensions, fasteners, shafts, windows, cable entries, and pressure-resistant structures where the “Ex d” method is selected. | Flameproof joint measurements, pressure tests, non-transmission tests, enclosure drawings, and certified component records. | Suitable for containing an internal explosion and preventing flame transmission to the surrounding atmosphere when the certified construction is maintained. | Protection-method specific |
| Increased-Safety Protection | GB/T 3836.3-2021; IEC 60079-7 | Prevent arcs, sparks, and excessive temperatures through controlled insulation, creepage distances, clearances, terminal construction, and thermal protection. | Insulation tests, temperature-rise tests, creepage and clearance calculations, terminal inspection, and component approvals. | Often used for equipment that does not normally produce arcs or sparks under normal operation. | Protection-method specific |
| Intrinsic-Safety Circuits | GB/T 3836.4-2021; IEC 60079-11 | Limit electrical energy so that sparks or thermal effects cannot ignite the specified explosive atmosphere under defined fault conditions. | Entity parameters, loop calculations, fault analysis, galvanic-isolation data, barrier certificates, and system verification documents. | Commonly considered for sensors, communication circuits, measurement devices, and low-energy end effectors. | Circuit-level requirement |
| Dust Protection by Enclosure | GB/T 3836.31-2021; IEC 60079-31 | Prevent combustible dust ingress and control the maximum surface temperature of the enclosure and exposed components. | Dust-ingress tests, enclosure construction records, temperature tests, gasket specifications, and cleaning instructions. | Important for applications involving powders, grain, plastics, pharmaceuticals, chemicals, or other combustible dusts. | Dust-area requirement |
| Surface Temperature Control | GB/T 3836.1-2021; IEC 60079-0 | Ensure the maximum surface temperature remains below the ignition temperature of the relevant gas, vapor, mist, or dust under the specified ambient and load conditions. | Thermal calculations, full-load temperature-rise tests, ambient-temperature limits, and temperature-class or maximum-surface-temperature marking. | Motors, brakes, drives, batteries, lighting, and charging interfaces require particular attention because they can generate heat. | Required for certification |
| Ingress Protection | GB/T 4208-2017; IEC 60529 | Specify an enclosure protection rating appropriate to dust, water, cleaning procedures, chemicals, and the robot’s intended environment. | IP test report, enclosure drawings, gasket and sealing specifications, cable-entry details, and maintenance instructions. | Ingress protection is not a replacement for explosion protection; both requirements must be satisfied independently. | Environmental requirement |
| Robot Motion and Control Safety | GB/T 16855.1-2018; GB/T 15706-2012; applicable robot safety requirements | Implement risk-reduction measures for unexpected motion, emergency stopping, safe speed, protective stops, safety-related control systems, and loss of communication. | Risk assessment, safety-function specifications, Performance Level calculations, validation reports, and control-system test records. | Explosion protection does not replace functional safety. A robot must address both ignition prevention and personnel protection. | Dual safety obligation |
| Motors, Drives, and Braking Systems | Applicable GB/T 3836 protection method and relevant electrical product standards | Ensure motors, servo drives, brakes, reducers, connectors, and feedback devices are covered by the selected Ex protection concept and operating limits. | Component certificates, thermal test results, electrical schematics, fault analysis, and compatibility verification for the complete robot assembly. | Replacing a certified component with a non-equivalent part can invalidate the certified protection concept. | Assembly-level control |
| Battery and Charging Safety | GB/T 3836 series; applicable battery, charger, and hazardous-location requirements | Evaluate battery cells, battery-management systems, connectors, charging contacts, thermal runaway risks, ventilation, and energy isolation within the hazardous area. | Battery safety test reports, BMS protection logic, charging risk assessment, thermal analysis, and Ex certification scope. | Charging should normally be controlled outside the hazardous area unless the complete charging arrangement is specifically designed and certified for that location. | Application-dependent |
| Cable Glands and Interfaces | GB/T 3836.1-2021; GB/T 3836.15-2017; IEC 60079-14 | Use suitable certified cable glands, plugs, connectors, flexible conduits, and termination methods that preserve enclosure integrity and the selected protection type. | Gland certificates, installation torque records, cable compatibility data, sealing inspection, and wiring diagrams. | Dynamic robot joints require special attention to flexing, abrasion, bend radius, shielding, and protection continuity. | Installation-critical |
| Installation and Commissioning | GB/T 3836.15-2017; IEC 60079-14 | Install, select, and erect electrical equipment according to the hazardous-area classification, Ex marking, circuit parameters, earthing, bonding, and environmental conditions. | Installation inspection checklist, as-built drawings, torque records, grounding tests, cable-entry inspection, and commissioning report. | Correctly certified equipment can become unsafe if installed with unsuitable glands, wiring, grounding, or accessories. | Site requirement |
| Inspection and Maintenance | GB/T 3836.16-2017; IEC 60079-17 | Maintain the certified construction, inspect flameproof joints and seals, verify cable entries, monitor corrosion and damage, and control modifications. | Initial and periodic inspection records, maintenance schedules, repair logs, calibration records, and authorized replacement-part lists. | Inspection frequency and detail should reflect the equipment type, environment, duty cycle, and site risk assessment. | Lifecycle requirement |
| Repair and Overhaul Control | GB/T 3836.13-2021; IEC 60079-19 | Repair, overhaul, reclamation, and modification must preserve the original explosion-protection characteristics and use technically controlled procedures. | Repair authorization, dimensional inspection, replacement-part traceability, post-repair testing, and updated technical records. | Unauthorized machining, repainting, drilling, sealing changes, or component substitutions may compromise certification. | Controlled activity |
| China Market Certification | Applicable Chinese Ex-product certification and China Compulsory Certification requirements | Determine whether the complete robot, individual modules, or associated electrical equipment falls within the applicable Chinese certification scope for the intended market and use. | Valid certification certificate, Ex marking, certification scope, test reports, factory quality-assurance records, and product consistency documentation. | Certification scope should correspond to the actual robot configuration, protection method, ambient range, gas or dust group, and permitted installation zone. | Market-access check |
| Technical Documentation and Marking | GB/T 3836 series; applicable certification rules | Provide clear Ex marking, electrical ratings, ambient-temperature range, special conditions of use, installation restrictions, warnings, and maintenance instructions. | Nameplate artwork, user manual, declaration or certificate, controlled drawings, bill of materials, and special-condition register. | The marking must allow users and inspectors to verify that the robot is suitable for the specific hazardous location. | Documentation requirement |

China Best Explosion Proof Robot Manufacturer?
Evaluating a Chinese explosion-proof robot manufacturer requires more than comparing prices. Examine its engineering records, factory controls, and application experience. Ask for complete product documentation, including hazardous-area ratings, enclosure protection, temperature limits, payload data, and battery safety details. Certificates should match the intended environment, not merely appear in a sales presentation.
Visit the production site when possible. Observe wiring, sealing, surface finishing, and final inspection procedures. Ask how each unit is traced from component purchase to shipment. A reliable manufacturer should explain testing equipment, calibration intervals, and failure-handling procedures clearly. Request sample inspection reports and verify them with qualified certification bodies. Real customer references also matter, especially from dusty, humid, or chemically demanding workplaces.
During a pilot review, test the robot under realistic conditions. Check climbing ability, camera clarity, remote response, emergency stopping, and operating time. Do not accept laboratory claims without field evidence. A polished factory tour can still hide weak after-sales support. I once underestimated spare-part response time; the robot performed well, but a delayed replacement stopped the trial. That mistake remains useful. Evaluate training, software updates, maintenance access, and technical communication before signing an agreement. The strongest supplier is not always the cheapest or most impressive. It is the one that documents limitations honestly and improves them through measurable engineering work.
Temperature-class capability is a key technical indicator when evaluating an explosion-proof robot manufacturer. The maximum surface temperature of the robot must remain below the ignition temperature of the surrounding hazardous gas or vapor.
Evaluation guidance: Ask the manufacturer to provide valid explosion-protection certificates, test reports, equipment-group information, gas-group classification, temperature class, ingress-protection rating, and documentation showing that the complete robot system—not only individual components—meets the required hazardous-area specification.
Designing an explosion-proof robot requires more than sealing a standard machine. The enclosure must control ignition risks, heat, pressure, and static discharge.
Engineers begin with the worksite. They study gas or dust hazards, aisle width, surface conditions, and operator distance. Small details matter. A sharp frame edge can damage protective cables.
Reliable design uses certified electrical parts, controlled flame paths, and carefully selected battery systems. Cameras, motors, sensors, and communication modules need compatible protection levels. Thermal modeling helps prevent hot surfaces during long shifts. Yet models are never perfect. Actual dust, moisture, and vibration can expose weaknesses that simulations miss.
Testing should reflect real work, not only laboratory conditions.
Teams can perform ingress checks, vibration tests, drop tests, brake trials, and extended runtime evaluations. Temperature monitoring is essential. So is inspection after repeated charging cycles.
Independent laboratory assessment and complete test records improve confidence. Customization then connects the robot to a specific task.
Options may include tracked mobility, robotic arms, gas detection, low-light cameras, or remote data links. Payload changes affect balance and battery life. A larger camera is not always better.
Field trials should confirm turning clearance, signal stability, and emergency shutdown response. Some designs need revision after the first trial. That is not failure; it is useful evidence.
Selecting an explosion-proof robot requires more than comparing prices. The International Federation of Robotics reported 541,302 industrial robot installations worldwide in 2023. Demand is growing, but hazardous-area projects require stricter evidence. Ask for certification scope, gas or dust classification, temperature rating, ingress protection, and payload test records. IECEx or ATEX documentation should match the complete robot system, not only one component. Small details matter.
During procurement, request sample inspection reports, wiring diagrams, spare-part lists, and operator training plans. Confirm whether the supplier can support factory acceptance testing and on-site commissioning. Installation teams should verify grounding, cable glands, ventilation, and emergency-stop interfaces before production starts. The IFR’s World Robotics 2024 report recorded more than 4.28 million industrial robots operating globally in 2023, yet installation quality still determines practical reliability. A certified robot can fail operationally when integration is rushed.
Lifecycle support deserves equal attention. Define response times, remote diagnosis procedures, preventive maintenance intervals, and software update controls in the contract. Keep critical seals, sensors, and cables available locally where possible. Track temperature, vibration, cycle time, and fault history from the first month. This data exposes hidden wear. A 2024 manufacturing technology survey by Deloitte also identified skills shortages as a major implementation challenge, so training cannot be treated as an optional extra. My practical concern is simple: many purchasing teams evaluate the machine carefully, but underestimate five years of support costs.